Consumables Lifecycle Engineering: When to Replace, Rotate or Repair to Protect Cost-Per-Metre
On many drill sites, consumables are managed with a simple rule:
Use it until it fails. Replace it when it breaks.
At first glance, that approach appears economical. But in mineral exploration and production drilling — particularly across remote African operations — reactive replacement increases non-productive time, destabilises cost-per-metre, and compounds logistics risk.
Drill rods, bits, reaming shells, and couplings do not fail randomly. They degrade progressively. When lifecycle control is absent, small wear patterns escalate into string failure, hole deviation, retrieval operations, and emergency freight.
Drilling consumables lifecycle management is not about extending component life indefinitely.
It is about engineering predictable replacement to protect production economics.
This Field Notes article examines how lifecycle engineering — rather than reactive habit — stabilises cost-per-metre across African drill programs.
The Hidden Cost of “Run It Until It Fails”
Consumables are often viewed as variable costs. But unmanaged wear transforms them into downtime multipliers.
When a rod fails unexpectedly:
- The drill string must be retrieved.
- The hole may collapse.
- The crew waits.
- Replacement components may not be immediately available.
- Emergency freight may be required.
The failure cost far exceeds the component cost.
Reactive replacement creates:
- Unplanned downtime
- Increased MTTR
- Emergency logistics
- Increased risk of secondary damage
By contrast, drilling consumables lifecycle management converts unpredictable failure into planned maintenance.
Mean Cycles to Failure: Engineering the Data
The first step in lifecycle control is measuring Mean Cycles to Failure (MCF).
MCF represents the average number of operational cycles a consumable can endure before reaching engineered retirement thresholds.
For drilling operations, this may include:
- Rod make-and-break counts
- Bit running hours
- Reaming shell operating hours
- Thread engagement cycles
Why Manufacturer Lifespan Is Not Enough
Manufacturer guidelines provide baseline expectations. However, actual lifecycle varies according to:
- Ground hardness
- Abrasiveness
- Torque discipline
- Operator technique
- RPM stability
- Environmental conditions
African drill programs often operate across variable geology — from fractured formations to abrasive hard rock — meaning site-specific data must inform drilling consumables lifecycle management.
Tracking cycles allows sites to:
- Identify early degradation patterns
- Predict retirement windows
- Schedule replacements proactively
- Reduce catastrophic failure probability
Consumables degrade predictably under load.
Lifecycle data transforms that degradation into engineering intelligence.
Thread Wear Tolerances: Engineering Limits vs Visual Guesswork
Thread failure is one of the most expensive consumable breakdown events.
Yet thread condition is often assessed visually:
“It still looks usable.”
That is not an engineering standard.
Thread degradation includes:
- Galling
- Microfracture formation
- Deformation under repeated torque
- Surface fatigue
Engineering Wear Thresholds
Proper drilling consumables lifecycle management defines:
- Maximum allowable pitch distortion
- Tolerance loss percentage
- Crest rounding thresholds
- Engagement depth limits
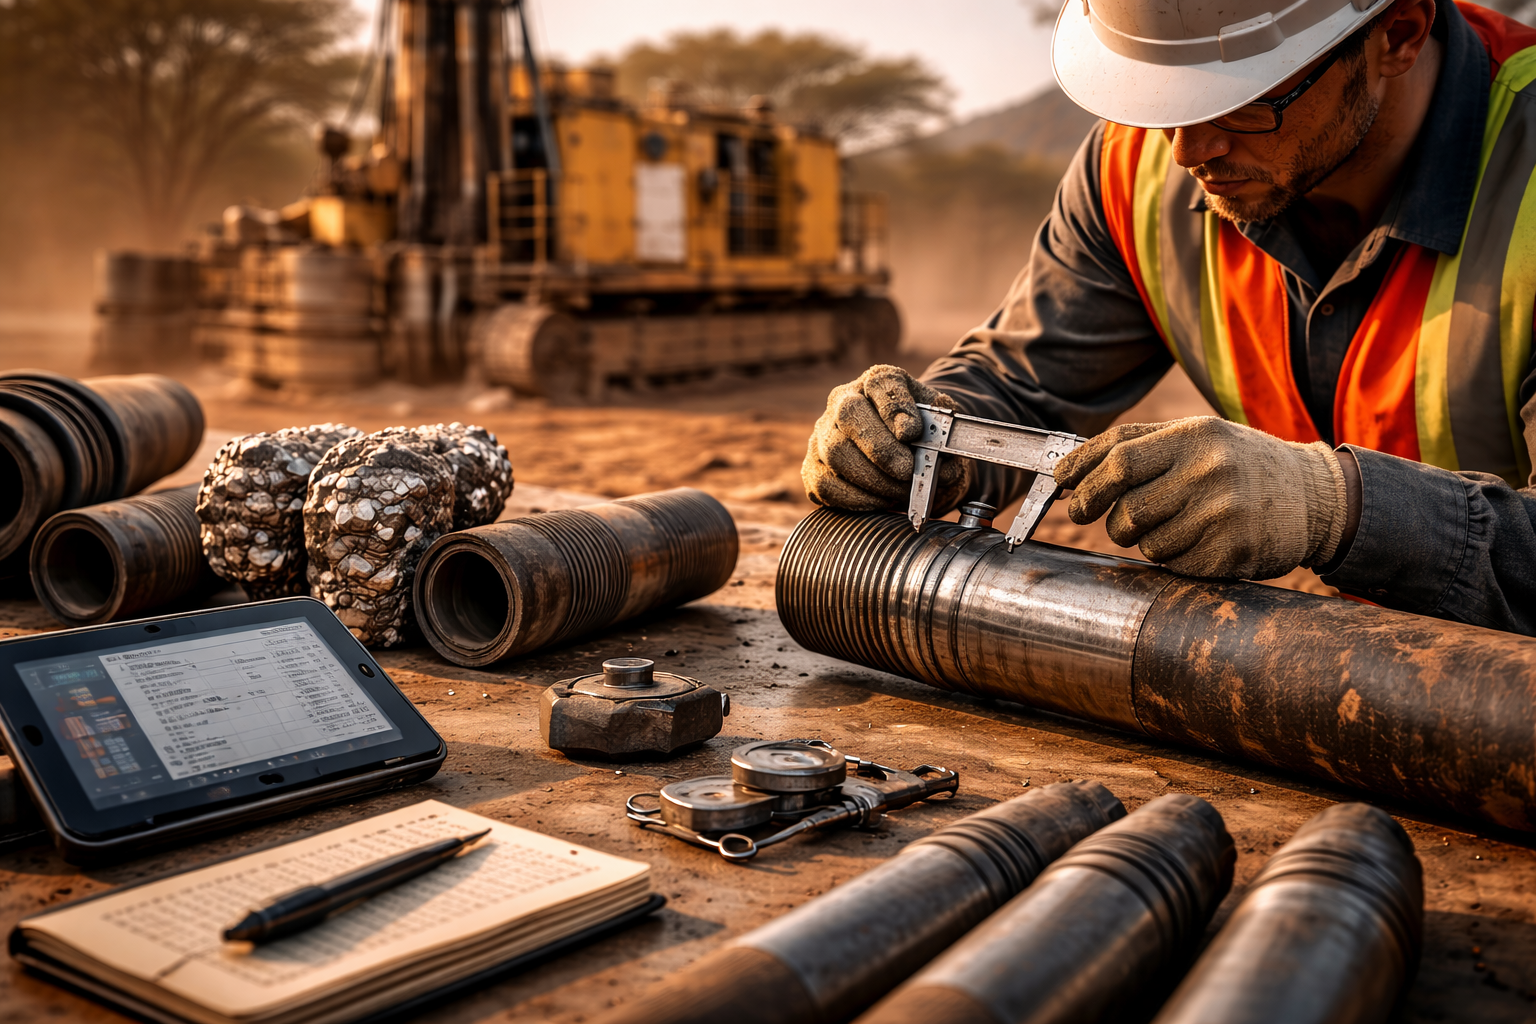
Using thread gauges and structured inspection tools allows crews to classify wear into tiers:
Tier 1: Within tolerance
Tier 2: Approaching retirement
Tier 3: Remove from service
Without tolerance measurement, threads are retired too late — often during load — resulting in string failure.
This connects directly with lessons discussed in Thread Damage & Rod Failure, where early warning signs prevent catastrophic downtime.
Inspection Intervals and Structured Monitoring
Inspection is not a once-a-week activity.
It must reflect operational intensity.
Inspection intervals should be calibrated according to:
- Ground conditions
- Torque levels
- Load intensity
- Number of daily cycles
- Environmental exposure
Recommended Discipline Framework
Daily:
- Visual inspection of threads and shoulders
- Surface contamination removal
- Immediate isolation of suspect components
Weekly:
- Tolerance measurement
- Detailed thread inspection
- Recording wear progression
Cycle-Based:
- Retirement triggers based on MCF
- Scheduled rotation before failure threshold
Structured inspection transforms drilling consumables lifecycle management from assumption into measurable control.
Predictive vs Reactive Replacement
The difference between predictive and reactive replacement determines program stability.
Reactive Replacement
- Replace after visible failure
- Unplanned downtime
- Emergency freight
- String retrieval operations
- Potential hole collapse
Predictive Replacement
- Replace at engineered threshold
- Scheduled downtime window
- Parts prepared in advance
- Lower stress on crew
- Stabilised drilling rhythm
Predictive systems reduce:
- MTTR
- Emergency logistics cost
- Downtime modelling risk
As explored in Cost-Per-Meter Reality, stability in drilling output protects economic performance.
Lifecycle engineering is production protection.
Stock Rotation Strategy: Extending Lifecycle Value
Drilling consumables lifecycle management extends beyond the rig floor.
Poor stock discipline erodes consumable integrity before use.
Key risks include:
- Corrosion due to moisture exposure
- Seal deterioration in high heat
- Dust contamination
- Shelf-life degradation
FIFO Discipline
First-In, First-Out rotation prevents aging stock from degrading unused.
Storage Engineering
Proper lifecycle control requires:
- Covered storage
- Humidity management
- Corrosion protection
- Thread protectors
- Regular inventory audits
Overstocking introduces risk:
- Components degrade in storage
- Capital is tied up
- False sense of availability masks poor rotation
This aligns closely with structured inventory principles outlined in Consumables Inventory Strategy for Remote African Drill Sites.
Lifecycle control and inventory engineering are interdependent.
African Operating Realities
Drilling programs across Africa face environmental pressures that accelerate wear:
- High ambient temperatures
- Dust infiltration
- Remote transport vibration
- Inconsistent technician availability
- Variable operator skill levels
These factors shorten effective lifespan if lifecycle engineering is not disciplined.
Ground variability also impacts degradation rate:
- Hard rock increases torque stress
- Fractured formations increase vibration
- Abrasive geology accelerates bit wear
Drilling consumables lifecycle management must account for these variables — not rely solely on manufacturer specifications.
The Compounding Cost-Per-Metre Impact
Consider a program where premature rod failure increases by just 5%.
The consequences include:
- Increased string retrieval events
- Re-drilling requirements
- Increased NPT
- Higher wear on adjacent components
- Delayed geological reporting
Now extend that across a multi-month campaign.
Small inefficiencies compound.
A 5–10% reduction in catastrophic consumable failures can materially stabilise cost-per-metre.
Lifecycle engineering is not about maximising lifespan.
It is about optimising replacement timing.
Repair vs Retire: Making the Correct Call
Some consumables can be:
- Re-cut
- Refaced
- Repaired
Others should be retired.
Engineering discipline requires:
- Defined repair criteria
- Maximum number of reconditioning cycles
- Documented inspection history
Repair without lifecycle tracking creates hidden fatigue risk.
Retire too early, and cost increases.
Retire too late, and downtime increases.
Drilling consumables lifecycle management finds the balance point.
Lifecycle Data as a Management Tool
Sites that implement structured lifecycle control gain:
- Predictable ordering schedules
- Reduced emergency freight
- Lower catastrophic failure rates
- More accurate cost-per-metre forecasting
- Improved inventory planning
Lifecycle tracking also supports procurement discussions with evidence-based data rather than anecdote.
It converts consumables from reactive expense into managed assets.
Field Notes Close
Consumables do not fail unpredictably.
They degrade progressively — and predictably — under load.
When degradation is unmanaged:
- Downtime increases
- Emergency freight multiplies
- Cost-per-metre rises
- Crew productivity suffers
When lifecycle engineering is structured:
- Replacement timing becomes predictable
- Downtime risk reduces
- Inventory stabilises
- Production output becomes more consistent
Drilling consumables lifecycle management is not about extending lifespan indefinitely.
It is about controlling degradation before it controls your program.
Before placing your next consumables order, evaluate:
Do you know your mean cycles to failure?
Do you measure thread wear tolerances?
Do you rotate stock properly?
If not, the first failure has already begun.
Frequently Asked Questions
1. What is drilling consumables lifecycle management?
Drilling consumables lifecycle management is the structured tracking, inspection, and predictive replacement of drill rods, bits, and related components based on measurable wear and cycle data rather than reactive failure.
2. How do you calculate mean cycles to failure?
Mean cycles to failure are calculated by tracking operational cycles (such as make-and-break counts or running hours) until retirement across multiple components, then averaging those values under similar operating conditions.
3. When should drill rods be replaced?
Drill rods should be replaced when thread wear approaches engineered tolerance thresholds or when recorded cycle counts approach established retirement benchmarks, not when visible failure occurs.
4. What are acceptable thread wear limits?
Acceptable thread wear limits depend on manufacturer specifications, but measurable deformation, crest rounding, pitch distortion, and engagement depth loss beyond defined tolerance thresholds indicate retirement.
5. How does stock rotation affect consumable lifespan?
Improper stock rotation leads to corrosion, moisture damage, and degradation before use. FIFO discipline and proper storage protect consumable integrity and extend effective lifecycle performance.