Bit Selection and Matrix Management: How to Stop Burning Bits and Stabilise Cost-Per-Metre in African Ground
A programme starts well. Metres advance at acceptable rates. Recovery is within tolerance. Shift reports look clean.
Then consumable costs begin to climb.
Bits are coming out earlier than expected. Penetration rate drops suddenly. Torque rises progressively. Vibration increases. The core becomes more fragmented at certain intervals. The report notes “abrasive ground” and “difficult formation.”
Ground is blamed. But the pattern repeats in the next hole.
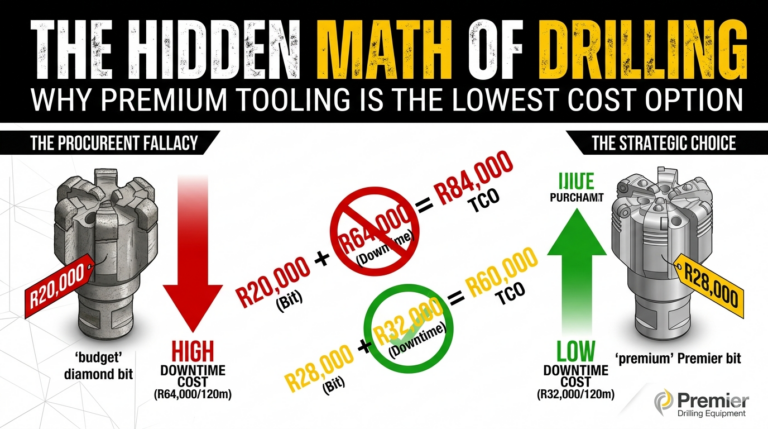
In most cases, premature bit wear is not random. It is a mismatch between formation, matrix hardness, and drilling parameters. Diamond drill bit selection for African operations does not depend on brand preference. It is about system compatibility.
Bit life is not controlled by the bit alone. It is controlled by how the bit, matrix, parameters, and formation interact.
What the Bit Is Actually Doing in the Hole
A diamond bit does not simply “cut rock.” It manages controlled abrasion and controlled diamond exposure.
The matrix holds industrial diamonds in place. As drilling progresses, the matrix wears gradually, exposing fresh diamonds at a controlled rate.
- If the matrix wears too slowly, diamonds polish and glaze.
- If it wears too quickly, diamonds are lost before they can cut effectively.
The bit must:
- Cut efficiently without excessive heat
- Release worn diamonds at the correct rate
- Maintain stability under rotation and feed pressure
- Clear-cuttings effectively
When this balance is correct:
- Torque remains stable
- Penetration is consistent
- Core recovery remains predictable
When the balance is incorrect, torque increases, vibration rises, and the cost-per-metre begins to rise quietly.
The Main Failure Modes Crews Misdiagnose
Glazing and Polishing
Glazing occurs when the matrix is too hard for the formation. Diamonds become blunt but remain trapped in the matrix. Instead of cutting, the bit begins grinding.
Common signs include:
- Rapid torque increase
- Reduced penetration rate
- Smooth, shiny bit face
- Increased heat
Glazing is often mistaken for “very hard rock.” In reality, the matrix is not wearing fast enough to expose fresh diamonds.
Premature Wear in Abrasive Horizons
In quartz-rich or highly abrasive formations, a soft matrix may wear too quickly. Diamonds are lost before delivering full cutting life.
This leads to:
- Rapid bit diameter reduction
- Shortened run lengths
- Frequent bit changes
- Increased consumable cost
Abrasive formation drilling requires correct matrix hardness to stabilise bit life.
Under-Exposure vs Over-Exposure
Matrix performance must match formation behaviour:
- Under-exposure: matrix too hard → diamonds glaze → torque rises
- Over-exposure: matrix too soft → diamonds shed early → bit life shortens
Both conditions increase the cost per metre drilled.
Cuttings Packing and Bit Loading
Poor flushing and excessive feed pressure can cause cuttings to pack around the bit face. This increases friction and heat and can trigger fast wear or burn events.
Symptoms include:
- Sudden torque spikes
- Sluggish rotation
- Heat discolouration
- Poor return flow
This is often diagnosed as a “bad bit,” when parameter discipline is the root cause.
Bit Burn Events
A “burned bit” is rarely a single moment. It is usually caused by a combination of:
- High RPM under rising torque
- Excessive feed in fractured ground
- Poor cooling and circulation
- Running a glazed bit too long
Burn events are system failures, not product failures.
How to Choose the Right Matrix for African Conditions
Matrix hardness must align with formation behaviour, not just “rock type on paper.”
In Competent Hard Rock
- Medium to hard matrix often performs well
- Stable feed pressure can be maintained
- Diamond exposure must be controlled to avoid polishing
In Fractured or Broken Ground
- A slightly softer matrix can improve exposure and reduce glazing risk
- RPM must be moderated to reduce vibration and core fragmentation
- Run length should be reduced to limit grinding and cutting accumulation
In Abrasive Quartz-Rich Zones
- A harder matrix is typically required
- Monitor the diameter wear closely
- Control RPM and flushing to reduce excessive heat
Standardising one bit across multiple lithologies is one of the fastest ways to destabilise cost-per-metre.
Diamond drill bit selection for African programmes must be formation-specific and signal-driven.
Parameter Discipline That Extends Bit Life
Bit life is directly connected to RPM, feed, and torque discipline.
When torque begins rising:
- Reduce feed slightly.
- Monitor torque response.
- If torque stabilises, hold the adjusted parameters.
- If torque continues rising, reduce RPM moderately.
- Shorten run length in unstable or abrasive intervals.
Never increase feed to “push through” rising torque. That decision often converts a manageable condition into cutting packing, heat, and premature wear.
To optimise bit life:
- Avoid chasing penetration rate at the expense of stability
- Respond to torque trend drift early
- Reduce RPM in fractured ground
- Maintain stable flushing and cooling
- Pull and inspect before a glazed bit becomes a burn event
Drilling performance optimisation is achieved by managing the system, not forcing metres.
Consumables and Rig Suitability
Bit life does not exist in isolation.
High-quality, compatible consumable core drilling products help stabilise the entire cutting system by keeping rods, reaming shells, core barrels, and bits working as one. Mismatched or worn components amplify vibration and destabilise the bit face.
Rig alignment and structural rigidity also influence wear. Properly configured geotechnical drill rigs improve mast alignment and near-surface stability, reducing lateral stress that accelerates bit wear.
In confined environments, well-configured underground drill rigs support stable torque transmission and controlled rotation, which helps maintain predictable diamond exposure.
When equipment is correctly matched, torque stabilises, and vibration reduces. When equipment is mismatched, bit wear accelerates regardless of matrix selection.
Field Logging: The Only Way to Stop Repeating Bit Mistakes
Without structured logging, bit mistakes repeat hole after hole.
Every run should record:
- Formation description
- RPM range
- Feed pressure range
- Torque trend (not just peak value)
- Penetration rate
- Core recovery percentage
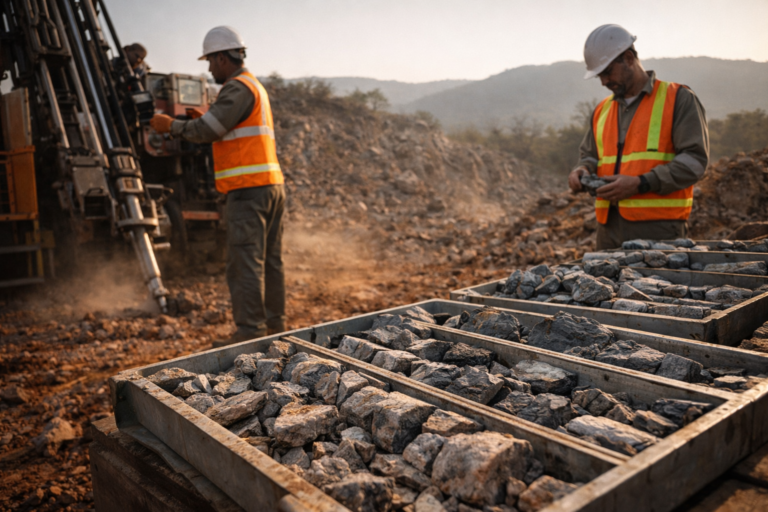
- Bit condition on removal (photo if possible)
Within two to three weeks, patterns emerge:
- Which matrix performs best in specific lithologies
- Where glazing consistently occurs
- Where abrasive wear accelerates
- What RPM window stabilises torque
- Which parameter responses prevent heat and packing
Logging converts assumptions into controlled adjustments.
The African Context
African drill programmes often operate in:
- Variable greenstone belts
- Mixed competent and fractured intervals within one hole
- Remote terrain with limited freight flexibility
- High-temperature, dusty environments
Water availability may fluctuate, affecting cooling and cutting transport. Formation transitions can occur rapidly within short depth intervals.
In remote operations, premature bit wear is more expensive because replacement timelines are longer. Preventing premature wear matters more when the resupply window is measured in days or weeks, not hours.
Conclusion: Bit Life Is a System, Not a Part
Bit failure is rarely random. It is the result of:
- Incorrect matrix selection
- Poor parameter discipline
- Incompatible consumables
- Inadequate logging
- Delayed response to torque drift
Correct diamond drill bit selection for African operations, combined with disciplined RPM/feed/torque control, is how you stop burning bits and stabilise cost-per-metre.
Optimise the life of the system by managing the system, not by blaming the formation.
When matrix hardness, parameters, equipment, and logging operate together, consumable burn reduces, torque stabilises, recovery improves, and programme predictability increases.
Frequently Asked Questions
How do I know if a bit is glazing?
If torque rises steadily while penetration rate drops and the bit face appears smooth and polished, glazing is likely. The matrix may be too hard for the formation, preventing fresh diamonds from being exposed.
What matrix hardness should I use in abrasive formations?
Abrasive, quartz-rich formations generally require a harder matrix to prevent premature diamond loss. RPM and feed must still be controlled to reduce heat and limit cutting packing.
Why does torque rise when a bit starts failing?
Torque rises when cutting efficiency declines. This can be caused by glazing, diamond loss, cutting, packing, insufficient flushing, or increasing friction due to instability.
How can I optimise the bit life on remote African drill sites?
Match matrix hardness to formation behaviour, maintain disciplined RPM and feed control inside a stable torque window, ensure compatible consumables across the string, and log every run consistently so performance patterns are corrected early.